 简体中文
 English
 русский
 Español

Home / News / Industry News / BLDC Silicon Steel Stator Core: Grade, Lamination Thickness and Sourcing
BLDC Silicon Steel Stator Core: Grade, Lamination Thickness and Sourcing
BLDC Silicon Steel Stator Cores: Grade, Gauge and Stacking
The steel grade, the sheet thickness and the way the laminations are held together decide more about efficiency, temperature rise and unit-to-unit consistency than any setting on the controller.
A 48 V brushless fan motor that should draw eight amps can read close to ten on the bench, and the driver board is rarely the reason. More often the stator core was made from 0.50 mm general-purpose steel where the electrical frequency called for 0.35 mm, or the interlocking dimples holding the stack together also formed a low-resistance bridge straight through it.
The conclusion first: grade, gauge and stacking method decide most of what a BLDC stator core will do, and the rest of the drawing only refines it. Grade sets core loss and permeability. Gauge decides how much of that loss survives at your electrical frequency, and what it costs in tooling life. Stacking method decides whether the laminations are still electrically separate after ten thousand units.
What follows is how to read a grade designation without being misled by its test conditions, when thin laminations earn their cost, what bonding and welding do to the magnetic circuit, and which numbers belong on the drawing before a purchase order goes out.
What a BLDC Stator Core Actually Has To Do
A stator core has three jobs: carry flux from the rotor magnets to the windings, do it with as little loss as the budget allows, and give the windings a rigid slot structure that survives varnish cure, thermal cycling and vibration.
Silicon is added to electrical steel mainly to raise resistivity, and resistivity suppresses eddy currents, the loss mechanism that grows with the square of frequency. That matters because a high pole count BLDC motor runs at a high electrical frequency even at modest shaft speed. A twelve-slot, fourteen-pole motor turning at 3,000 rpm sees roughly 350 Hz inside the core, while a four-pole motor at the same speed sees 100 Hz. Lamination does geometrically what silicon does chemically: slicing the core into thin insulated sheets stops circulating currents from building into one large loop.
- Hysteresis loss depends on the alloy and flux density, and is largely independent of sheet thickness.
- Eddy-current loss falls with the square of sheet thickness, which is why gauge matters more as frequency climbs.
- Stacking factor is the share of core volume that is actually steel rather than coating, adhesive or air, and it sets how much torque you get from a given stack height.
How To Read a Silicon Steel Grade
Non-oriented electrical steel grades carry their two key numbers in the name. In 35W270, the first two digits give nominal thickness in hundredths of a millimetre, so 0.35 mm, and the last three give guaranteed maximum core loss in watts per kilogram, so 2.70 W/kg. What the name does not tell you is the induction and frequency at which that loss was measured.
| Grade | Nominal thickness | Guaranteed loss | Typical BLDC fit |
|---|---|---|---|
| 50W600 | 0.50 mm | 6.00 W/kg at 1.5 T, 50 Hz | Cost-driven, low-speed fan and pump motors |
| 50W470 | 0.50 mm | 4.70 W/kg at 1.5 T, 50 Hz | General-purpose motors up to roughly 200 Hz |
| 35W300 | 0.35 mm | 3.00 W/kg at 1.5 T, 50 Hz | Mainstream BLDC, power tools, appliance motors |
| 35W270 | 0.35 mm | 2.70 W/kg at 1.5 T, 50 Hz | High-efficiency BLDC and servo cores |
| 20W1200 | 0.20 mm | 12.00 W/kg at 1.0 T, 400 Hz | High pole count traction and spindle cores |
The trap is comparing a figure taken at 1.0 T and 400 Hz against one taken at 1.5 T and 50 Hz. Eddy-current loss scales with the square of frequency, hysteresis loss scales roughly linearly, and both rise with induction, so a high-frequency grade always looks worse on paper even when it is the better material. A quotation should state loss at the induction and frequency your motor will actually run at, or include a full loss curve.
Lamination Thickness: Where Thin Actually Pays
Thinner is not automatically better and it is never free. Eddy-current loss falls with thickness squared, and that gain is real: dropping from 0.50 mm to 0.35 mm cuts the classical eddy component by roughly half at the same frequency and flux. Hysteresis loss does not fall with thickness, so as gauge drops the hysteresis share grows and the returns flatten out.
The downstream costs are easy to underestimate. More laminations for the same stack height means more strokes, faster die wear and more burr area to control. Stacking factor falls slightly, stack stiffness falls noticeably, and winding tension has to come down to avoid deforming the teeth. For a low-frequency, cost-sensitive motor, 0.50 mm steel is often the correct engineering choice rather than a compromise.
A workable starting point rather than a rule: below about 200 Hz, 0.50 mm is usually adequate. Between 200 and 400 Hz, 0.35 mm is the mainstream selection. Above 400 Hz, high pole count machines move to 0.27 mm or 0.20 mm.
Stacking Method Changes the Magnetic Circuit
How laminations are held together is an electromagnetic decision as much as a manufacturing one. Interlocking, welding, stapling and adhesive bonding each leave a different electrical fingerprint on the stack.
| Method | Inter-lamination insulation | Cycle time | Where it fits |
|---|---|---|---|
| Interlocking dimples | Lowest, each dimple is a metal bridge | Fastest | High-volume, lower-frequency cores |
| Welding on the outside diameter | Low along the weld seam | Fast | Rigid stacks where some eddy loss is acceptable |
| Stapling or cleating | Moderate, localised to the staple | Moderate | Larger cores needing mechanical strength |
| Adhesive bonding | Highest, full-surface insulation | Slowest, needs curing | High-frequency and traction cores |
Interlocking is the cheapest and quickest option and is entirely adequate for many low-frequency cores. Its weakness is that displaced metal at each dimple bridges adjacent laminations, and on a high-frequency core several hundred of those bridges add up. The result usually appears as higher no-load current rather than as a dimensional failure, which is why it can pass incoming inspection and still hurt.
Purchase risk to watch: a stack that measures perfectly in the prototype can drift in production if the supplier changes bonding pressure, anneal temperature or die maintenance interval between the sample and the first volume shipment.
Edge Quality, Annealing and the Losses Nobody Measures
Two cores can be dimensionally identical and still differ in loss by a margin that shows up clearly in temperature rise, because the difference lives in the edges and in the heat treatment.
Laser cutting is flexible and tooling-free, which makes it the default for prototypes and low volumes. It also leaves a heat-affected zone along the cut edge where the microstructure is altered and permeability drops. On a large core that band is negligible; on a small stator with narrow teeth it can be a meaningful fraction of the tooth width, and the tooth is exactly where flux density is highest.
Stamping with a sharp die produces a better magnetic edge but shifts cost into tooling and demands burr control. A burr limit around 0.05 mm is a common specification, because burrs both short laminations together at the edges and damage slot insulation during winding. The full lamination manufacturing sequence, from coil slitting to final annealing, is worth understanding before a process route is approved.
Stress relief annealing recovers much of the permeability lost to punching strain. On bonded stacks the sequence matters: heat treatment should finish before bonding, or the adhesive must be selected for the anneal temperature.
A core can pass every dimensional check and still run hot, because lamination-to-lamination insulation and edge stress never show up on a caliper.
What Belongs on the Drawing and in Incoming Inspection
The designer writes the tolerances, but the buyer has to read them, because on a stator core they define exactly what can drift in volume production.
- Bore diameter and concentricity to the outside diameter, since these two set the air gap.
- Tooth width at its narrowest point with a two-sided tolerance, because the tooth is the flux bottleneck.
- Slot width and depth, which control winding fill factor and leakage.
- Stack height and lamination count, referenced to a defined clamping pressure if the stack is compressed.
- Burr height limit, edge condition and which surfaces are critical.
- Squareness of the bore to the end faces, which affects rotor alignment and noise.
- Core loss on a sample, measured at the operating induction and frequency rather than at a catalogue condition.
Worth asking for: the process route as well as the drawing. Two suppliers can quote the same 35W270 material and the same tolerances and still deliver different cores if one anneals before bonding and the other does not.
Sample validation should follow a fixed sequence: prototype laminations, then a pilot lot from production tooling, then a capability study on the critical dimensions and a core loss check on a wound sample. Skipping the pilot lot is the most common cause of a design that measures well and then disappoints at volume. If that sequence needs to be planned around a specific motor programme, the engineering team can walk through it with you.
Where the Same Core Behaves Differently
Traction motors, appliance motors and servo motors all use BLDC silicon steel stator cores, and they ask for almost opposite things from the material.
Electric Vehicle Drive Motors
High pole counts push the electrical frequency well above a few hundred hertz, and the core has to survive deep thermal cycling without the bond line releasing. That combination points to 0.20 to 0.35 mm low-loss steel, adhesive bonding, and a loss figure measured at the real operating point.
Home Appliance and Power Tool Motors
Here the priorities reverse. Volumes are enormous, cost per core is measured in small fractions, and the electrical frequency is moderate. A 0.35 mm grade with interlocking or a light weld usually wins, provided the die is maintained well enough to hold burr height and tooth tolerance across a long run.
Servo and Precision Motors
Servo cores are judged on cogging torque, quiet running and repeatability more than on absolute loss. Slot and tooth tolerances tighten, skew has to be held precisely, and inter-lamination insulation has to stay uniform, because any asymmetry shows up as torque ripple the controller cannot fully hide.
What To Lock Down Before You Order
A BLDC silicon steel stator core is a specification problem before it is a manufacturing problem. Fix the grade against your real operating frequency, not against a catalogue condition. Fix the gauge against the loss you can actually measure, not against the thinnest steel you can afford. Fix the stacking method against the insulation quality the application needs, and write the burr limit, the anneal sequence and the core loss test into the purchase specification. Do those three things and the winding, the magnets and the controller can be designed with confidence, because the core will behave on the ten thousandth unit exactly as it did on the first sample.
Previous article
Motor core lamination process: Applications, Selection Criteria, and Practical Guidance
next article
Generator Stator Core Construction: Laminations, Stacking and Cooling Explained
Related News
-
What are Stator and Rotor Cores? Stator Cores A stator core is the stationary component of an electric motor. It's the part that houses the copper windings, which, when an electric current passes thro...
See Details -
Introduction The modern automobile is a complex machine, and its evolution has been driven by continuous innovation in every component. While internal combustion engines have dominated the industry fo...
See Details -
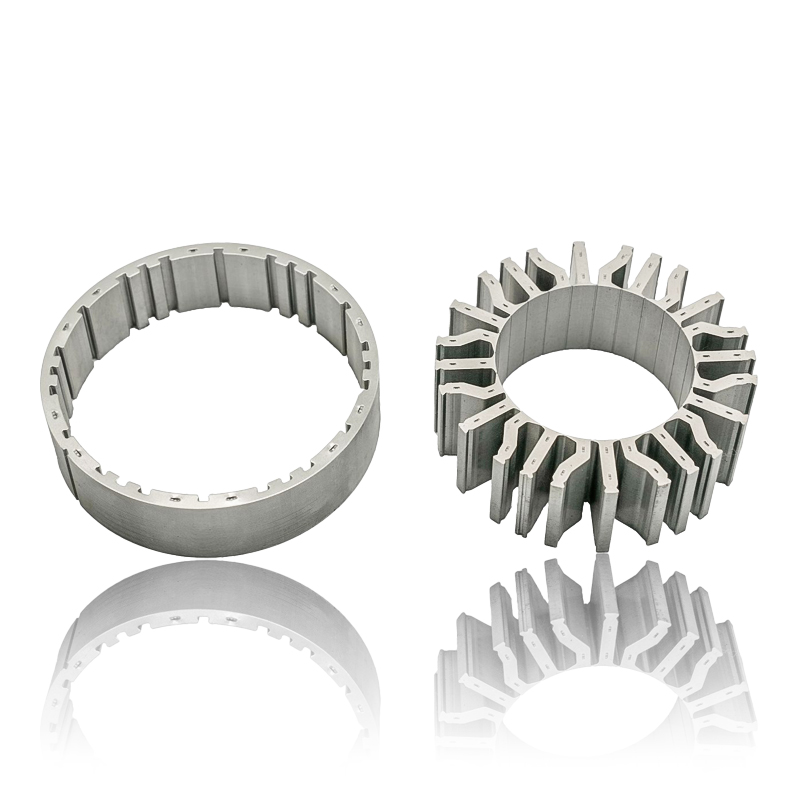
The Importance of Material Selection for Rotor and Stator Cores in Electric Vehicle Motors In the design of electric vehicle (EV) motors, material selection is a pivotal factor influencing the motor’s...
See Details -
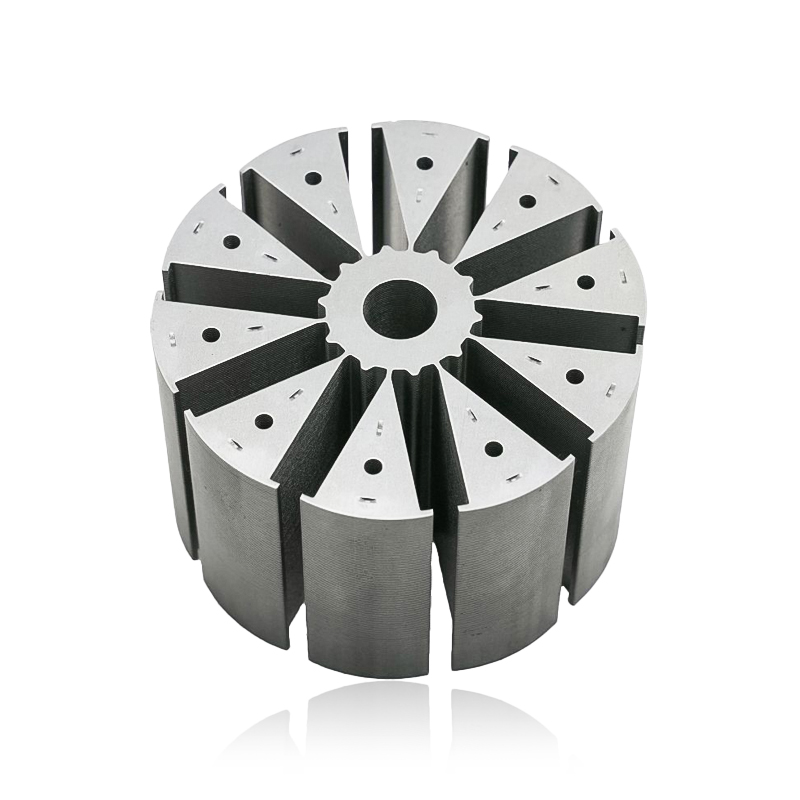
Introduction of automotive motor stator and rotor cores The increasing popularity of electric vehicles and hybrid electric vehicles has brought about significant advancements in automotive technology....
See Details
Zhejiang Jufeng Technology Co., Ltd. © All rights reserved
